Solid Liquid Separator Manufacturers in India - Dolphin Engineers
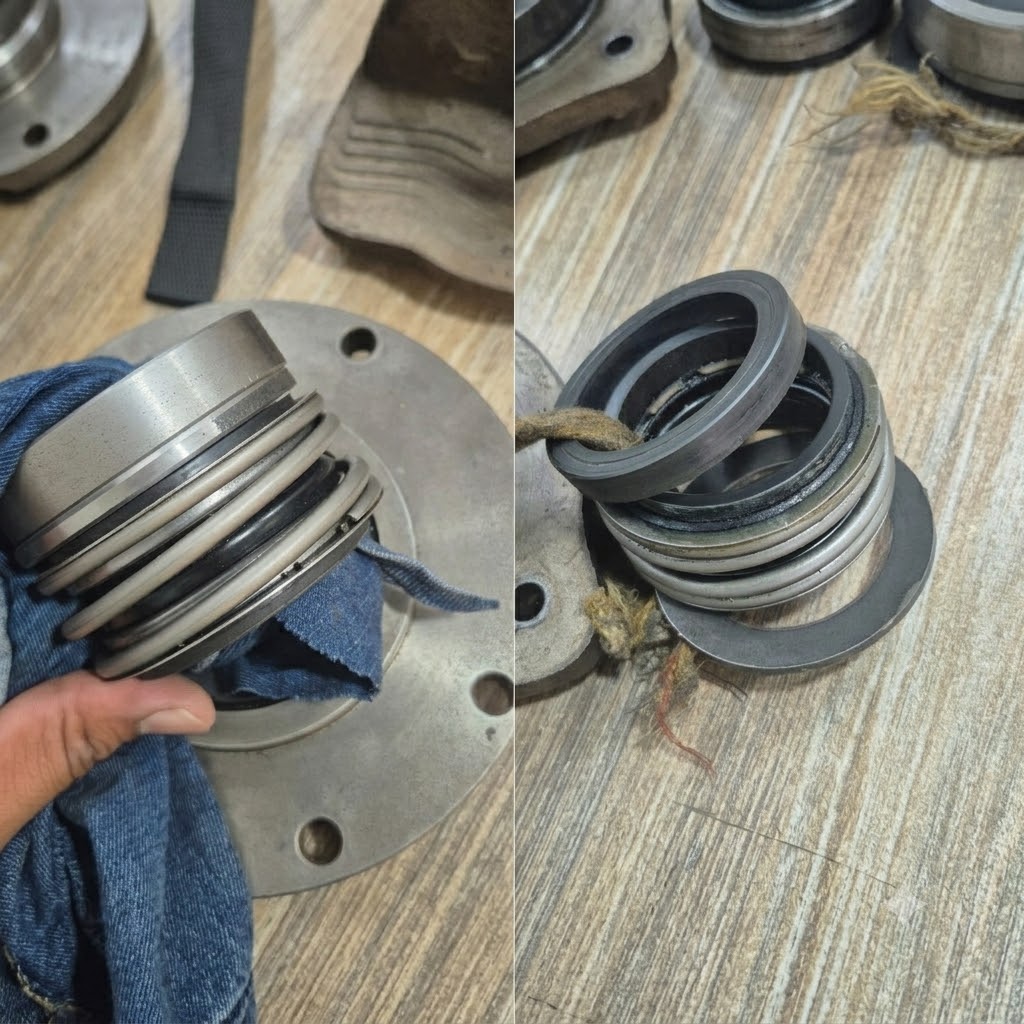
Dolphin Engineers is leading Solid Liquid Separator (SLS) Manufacturers, Suppliers, Dealers and Exporters in India. A Solid Liquid Separator (SLS) is an advanced industrial separation system designed to efficiently separate solid particles from liquid mixtures in continuous processing applications. It is widely used across industries where sludge, slurry, wastewater, or process liquids require effective separation for recovery, recycling, or disposal. An Industrial Solid Liquid Separator improves operational efficiency, reduces waste disposal costs, conserves valuable resources, and ensures compliance with environmental regulations.
Modern Solid Liquid Separation Machines are engineered for high-capacity operation, low maintenance, and consistent performance. Whether used for Sludge Dewatering, Wastewater Treatment, Food Processing, Chemical Manufacturing, or Mining Applications, these systems provide reliable and cost-effective solid-liquid separation solutions. At Dolphin Engineers, we manufacture and supply high-performance OEM Solid Liquid Separators that are customized to meet the specific requirements of different industries.
What is a Solid Liquid Separator?
A Solid Liquid Separator (SLS) is an industrial machine that separates suspended solid particles from liquids using mechanical or centrifugal force. The separated solids are discharged for disposal or reuse, while the clarified liquid can be recycled, treated further, or safely discharged.
A Solid Liquid Separation System plays a vital role in improving process efficiency, reducing environmental impact, and recovering valuable materials from industrial processes. These systems are available in various configurations, including Automatic Solid Liquid Separators, Continuous Solid Liquid Separators, and Heavy-Duty Industrial Solid Liquid Separators, depending on the application and material characteristics.
Industrial SLS equipment is commonly integrated into wastewater treatment plants, food processing facilities, mining operations, pharmaceutical manufacturing units, and chemical industries to achieve continuous and efficient separation.
Working Principle of a Solid Liquid Separator
The working principle of a Solid Liquid Separator involves separating materials based on differences in density, particle size, or centrifugal force.
- Material Feeding: The slurry, sludge, or liquid-solid mixture is continuously fed into the separator through the inlet system.
- Separation Process: Depending on the separator type, centrifugal force, filtration, or mechanical action separates heavier solid particles from the liquid phase.
- Solid Conveying: The separated solids are automatically conveyed toward the solids discharge outlet, allowing uninterrupted operation.
- Liquid Clarification: Clarified liquid flows through a separate outlet and can be reused, recycled, or sent for further treatment.
- Continuous Operation: Automatic control systems ensure continuous processing with minimal operator intervention, maximizing productivity and reducing downtime.
Types of Solid Liquid Separators
As we are leading Solid Liquid Separator Manufacturers in India, our Types are designed to meet different application requirements and industry standards, including the following types:
- 1. Industrial Solid Liquid Separator Designed for continuous industrial applications requiring efficient separation of solids from liquids under demanding operating conditions.
Applications:
- Wastewater treatment
- Chemical processing
- Food manufacturing
- Mining - 2. Automatic Solid Liquid Separator Fully automated systems equipped with intelligent controls for continuous operation, reduced labor, and improved process consistency.
Suitable For:
- Municipal treatment plants
- Industrial processing
- Pharmaceutical production - 3. Continuous Solid Liquid Separator Engineered for uninterrupted processing of large volumes of slurry, ensuring high throughput and maximum separation efficiency.
Applications:
- Sludge dewatering
- Industrial slurry processing
- Food processing - 4. Heavy-Duty Solid Liquid Separator Built for abrasive materials and high-solid-content applications using robust construction and wear-resistant components.
Ideal For:
- Mining
- Coal washing
- Mineral processing
- Oil & gas drilling - 5. OEM Solid Liquid Separator Custom-designed separation systems manufactured according to customer specifications, processing capacity, and industry requirements.
Available in:
- Stainless steel construction
- High-capacity models
- Customized automation
- Industry-specific configurations
Features of Solid Liquid Separator
As Solid Liquid Separator Suppliers in India, we have advanced features that ensure high precision, durability, and consistent performance.
- High Separation Efficiency: Our Solid Liquid Separators are engineered to deliver excellent separation performance, ensuring maximum recovery of solids while producing cleaner process liquids for reuse or discharge.
- Continuous Automatic Operation: The fully automatic design enables uninterrupted processing with minimal manual intervention, increasing productivity and reducing labor costs.
- Heavy-Duty Industrial Construction: Manufactured using premium-quality materials, the separator offers excellent durability, corrosion resistance, and reliable operation even in harsh industrial environments.
- Low Maintenance Design: Optimized mechanical components and wear-resistant construction reduce maintenance requirements, minimizing downtime and operating expenses.
- Energy-Efficient Performance: Advanced engineering and optimized drive systems reduce power consumption while maintaining high processing capacity and superior separation efficiency.
Benefits of Solid Liquid Separator
As Solid Liquid Separator Dealers in India, our products provide several benefits including consistent quality, smooth finish, and long service life.
- Improved Process Efficiency: Continuous solid-liquid separation enhances production efficiency by reducing process interruptions and increasing throughput across industrial operations.
- Reduced Waste Disposal Costs: By removing excess moisture from sludge and recovering valuable solids, industries can significantly reduce transportation and disposal expenses.
- Environmental Compliance: Efficient separation helps industries meet wastewater discharge regulations while supporting sustainable manufacturing practices and water recycling initiatives.
- Better Product Quality: Cleaner process liquids and effective removal of contaminants improve the quality of finished products in food, pharmaceutical, and chemical applications.
- Long-Term Cost Savings: Reliable operation, reduced maintenance requirements, lower energy consumption, and extended equipment life result in substantial long-term operational savings.
Industries We Serve
As Solid Liquid Separator Exporters in India, our all types are used in various types of industrial sectors such as:
| Industry | Application |
|---|---|
| Wastewater Treatment | Sludge Dewatering |
| Sewage Treatment Plants (STP) | Wastewater Processing |
| Effluent Treatment Plants (ETP) | Industrial Wastewater Treatment |
| Food Processing | Product Separation |
| Dairy Processing | Milk & Whey Clarification |
| Fruit Juice Industry | Juice Clarification |
| Edible Oil Processing | Oil Purification |
| Oil & Gas Industry | Drilling Mud Processing |
| Chemical Processing | Solid-Liquid Separation |
| Pharmaceutical Manufacturing | Product Recovery |
| Mining & Mineral Processing | Ore Slurry Processing |
| Coal Washing Plants | Coal Slurry Separation |
| Paper & Pulp Industry | Fiber Recovery |
| Sugar Processing | Juice Clarification |
| Brewery & Distillery | Beverage Clarification |
| Palm Oil Processing | Oil Recovery |
| Biofuel Production | Biodiesel Processing |
| Textile Industry | Wastewater Treatment |
| Industrial Slurry Processing | Solid Separation |
Why Choose Us?
- Industry Expertise: With years of experience in industrial separation technology, we provide reliable and efficient Solid Liquid Separation Systems tailored to diverse industrial applications.
- Customized OEM Solutions: We design and manufacture OEM Solid Liquid Separators based on customer-specific process requirements, capacity, material characteristics, and operational goals.
- Premium Quality Equipment: Our machines are manufactured using high-grade materials and precision engineering to ensure durability, high performance, and long service life.
- Advanced Engineering: Our separators incorporate modern technology for high separation efficiency, energy savings, automated operation, and reduced maintenance requirements.
- Comprehensive Technical Support: From equipment selection and installation to commissioning, maintenance, and after-sales service, our experienced technical team provides complete support throughout the equipment lifecycle.
- Competitive Pricing: We offer cost-effective Industrial Solid Liquid Separators without compromising on quality, performance, or reliability, delivering excellent value for your investment.
Choose Dolphin Engineers is leading Solid Liquid Separator (SLS) Manufacturers, Suppliers, Dealers and Exporters in India. A Solid Liquid Separator (SLS) is an essential solution for industries requiring efficient and continuous separation of solids from liquids. Whether used for Sludge Dewatering, Wastewater Treatment, Food Processing, Chemical Manufacturing, or Mining Applications, these systems improve operational efficiency, reduce waste management costs, and support sustainable industrial processes. At Dolphin Engineers, we deliver high-performance, OEM-quality Solid Liquid Separation Equipment designed to provide reliable performance, maximum productivity, and long-term operational benefits.
FAQ’s
A Solid Liquid Separator is an industrial machine used to separate suspended solid particles from liquids, producing clarified liquid and dewatered solids for disposal, recycling, or further processing.
The separator uses mechanical action, filtration, or centrifugal force to separate solids from liquids. The solids are discharged automatically, while the clarified liquid exits through a separate outlet.
These systems are widely used in wastewater treatment, sewage treatment plants (STP), effluent treatment plants (ETP), food processing, dairy, pharmaceuticals, chemicals, mining, paper & pulp, sugar, textile, oil & gas, biofuel, and palm oil industries.
Key benefits include high separation efficiency, reduced waste disposal costs, improved product quality, lower maintenance, energy savings, environmental compliance, and continuous automatic operation.
The ideal separator depends on factors such as slurry characteristics, particle size, processing capacity, moisture content, industry application, and automation requirements. A customized evaluation helps determine the most suitable solution.