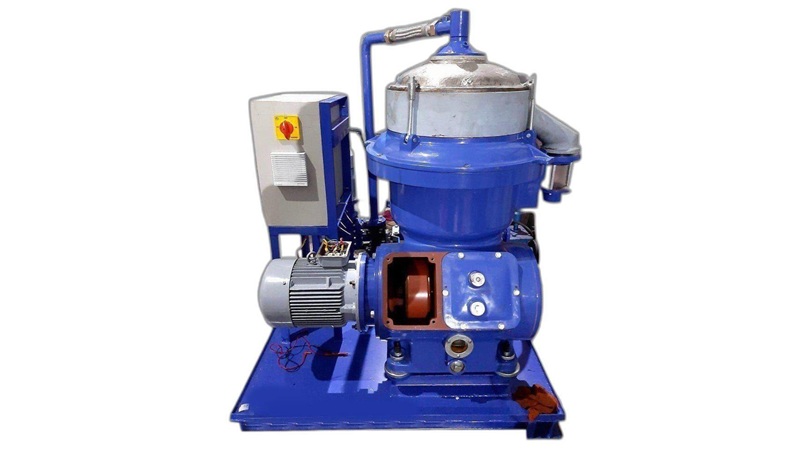
Centrifuge Machine
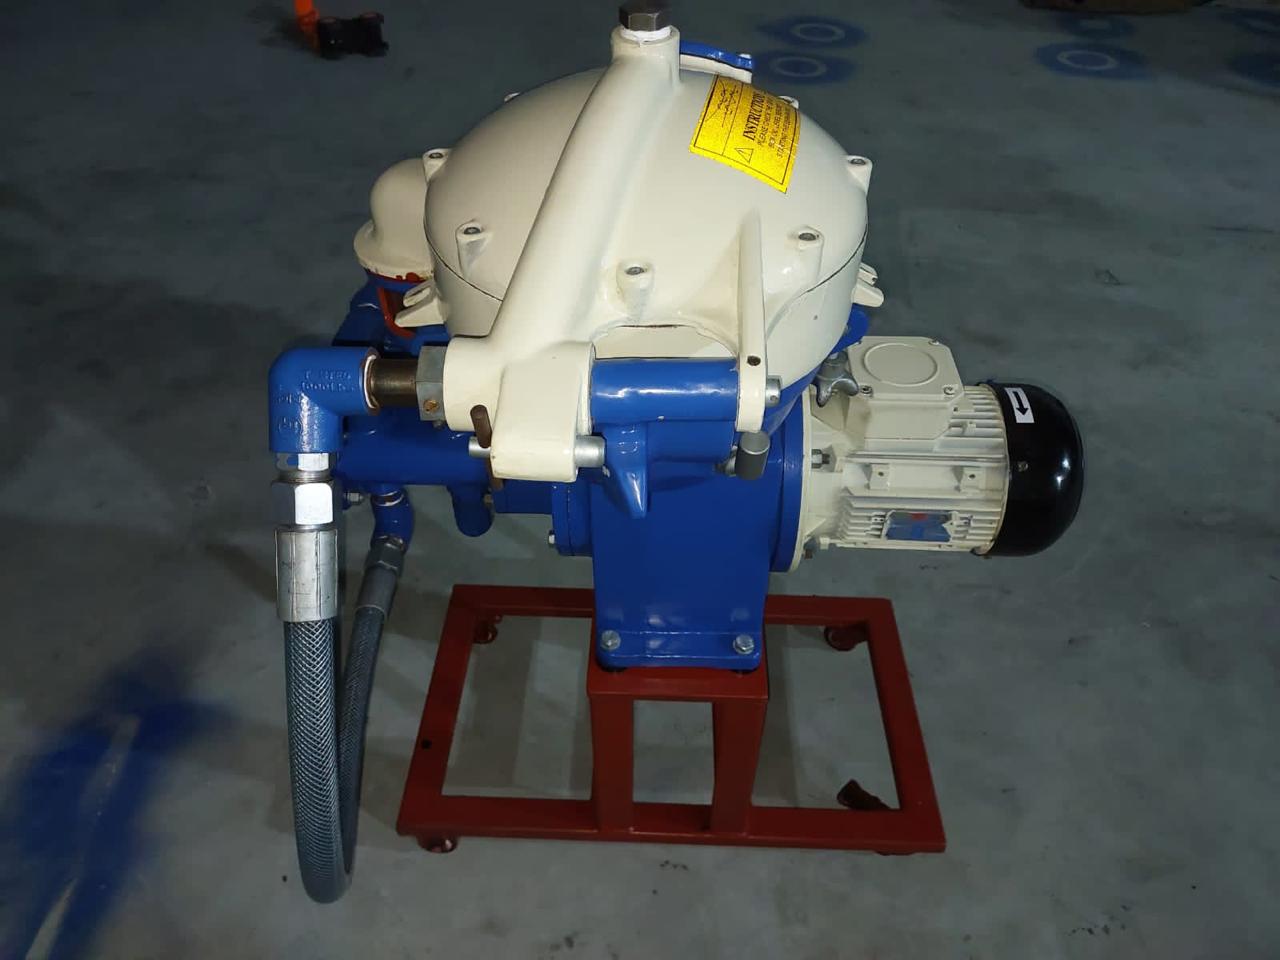
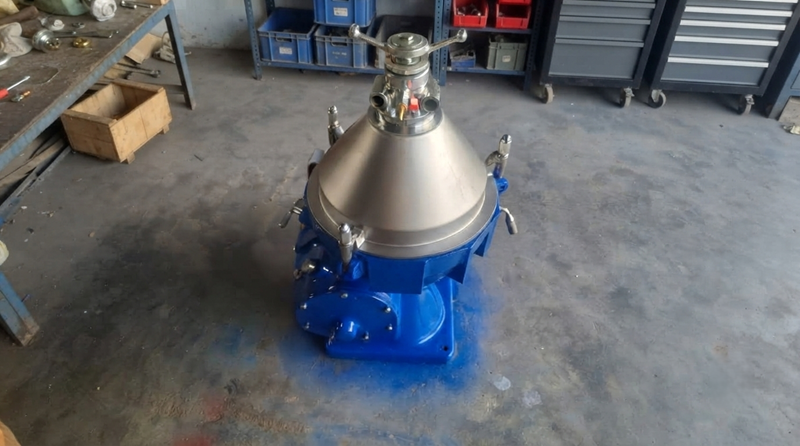
Our Centrifuge Machine is designed for efficient and continuous separation of solid and liquid components from process mixtures. Centrifuge machines use centrifugal force to achieve rapid separation and are widely used in industries where efficient clarification, dewatering, and solid-liquid separation are required.
We provide reliable centrifuge solutions designed to meet different industrial processing requirements. Depending on the application, material characteristics, capacity, and required separation performance, the appropriate centrifuge configuration can help improve process efficiency, reduce moisture content, and maintain consistent plant operations.
Efficient Separation
Uses high-speed centrifugal force to efficiently separate solids and liquids for improved process performance.
Continuous Operation
Designed for continuous industrial processes requiring reliable and consistent separation performance.
Robust Construction
Strong mechanical construction designed to withstand demanding industrial operating conditions.
High Process Efficiency
Helps improve separation efficiency, reduce processing time, and support optimized plant operations.
Working Principle of Centrifuge Machine
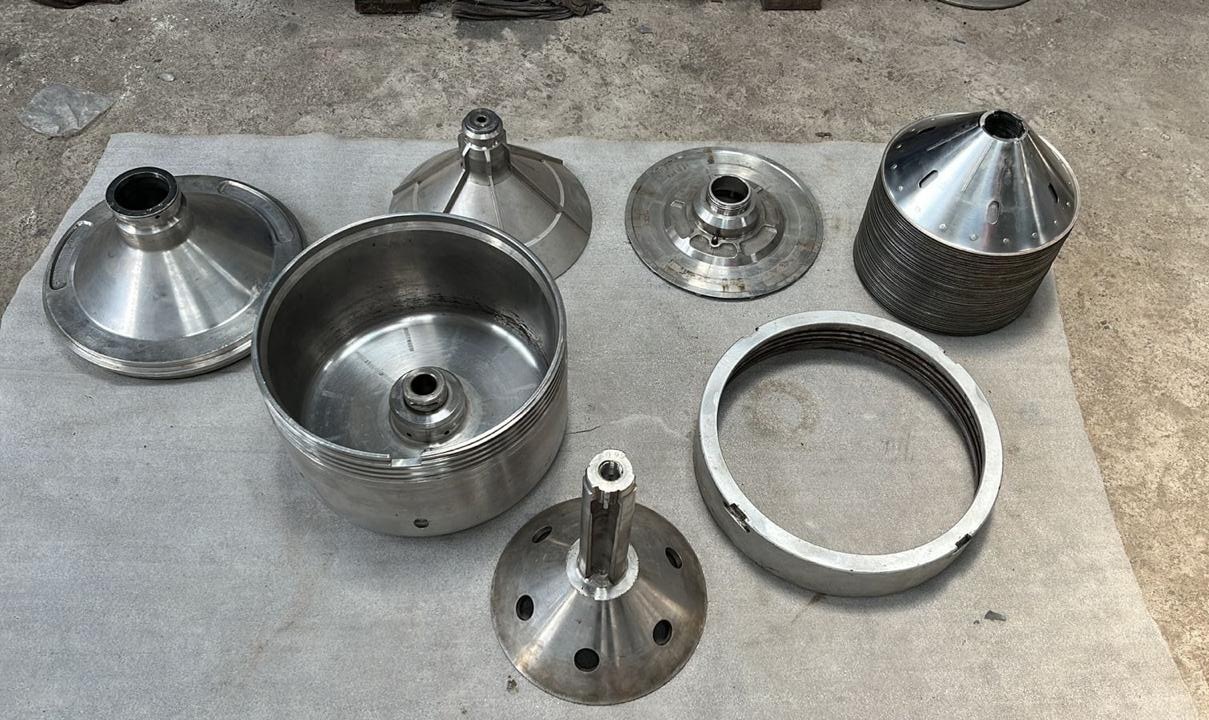
A centrifuge machine separates components of a process mixture by generating centrifugal force through high-speed rotation. When the mixture enters the centrifuge, the heavier particles move outward while lighter liquid components remain closer to the center of rotation.
The separated materials are then discharged through their respective outlets depending on the centrifuge design and application. Operating parameters such as rotational speed, feed rate, particle size, concentration, and material characteristics influence the overall separation performance.
- Process material feeding.
- High-speed centrifugal rotation.
- Separation of solid and liquid phases.
- Controlled material movement.
- Continuous separation process.
- Efficient solids discharge.
- Liquid clarification.
- Reduced moisture content.
- Improved downstream processing.
- Consistent process performance.
Types of Centrifuge Machines
Different types of centrifuge machines are available to meet specific separation requirements. The appropriate machine depends on the characteristics of the process material, required capacity, separation objective, solids concentration, and operating conditions.
- Decanter Centrifuge
- Disc Stack Centrifuge
- Basket Centrifuge
- Industrial Process Centrifuge
- Solid-Liquid Separation Centrifuge
- Sludge Dewatering Centrifuge
- Clarification Centrifuge
- High-Speed Centrifuge
- Continuous Centrifuge Systems
- Application-Specific Centrifuge Solutions
Applications of Centrifuge Machines
Centrifuge machines are widely used in industrial and process applications where rapid separation of solids and liquids is required. Their ability to provide continuous and efficient separation makes them suitable for a broad range of industries.
- Wastewater and sewage treatment.
- Industrial effluent treatment.
- Food and beverage processing.
- Chemical processing industries.
- Pharmaceutical processing.
- Oil and petrochemical industries.
- Mining and mineral processing.
- Sludge dewatering applications.
- Biofuel and renewable energy processes.
- General industrial separation.
Benefits of Centrifuge Machine
Centrifuge machines can provide significant advantages in industrial separation processes by delivering efficient separation within a relatively compact equipment footprint. Properly selected and operated centrifuges can contribute to improved productivity and reduced processing requirements.
- Efficient solid-liquid separation.
- Continuous processing capability.
- Reduced moisture in separated solids.
- Improved liquid clarification.
- Reduced downstream process load.
- Compact equipment arrangement.
- Improved process productivity.
- Reliable industrial operation.
Why Choose Our Centrifuge Machines?
Selecting the right centrifuge is essential for achieving the desired separation performance and maintaining reliable operation. Our approach focuses on understanding the application, process material, capacity requirements, and operating conditions before recommending a suitable centrifuge solution.
- Application-focused equipment selection.
- Efficient separation performance.
- Robust mechanical construction.
- Solutions for different industrial applications.
- Technical assistance and support.
- Reliable equipment performance.
- Maintenance and service support.
- Focus on long-term operational reliability.
Centrifuge Machine Maintenance
Regular inspection and preventive maintenance are important for maintaining the performance, reliability, and safety of centrifuge machines. Since centrifuges operate at high rotational speeds and under continuous mechanical loads, appropriate inspection and maintenance practices are essential.
Routine maintenance may include inspection of rotating components, bearings, seals, drive systems, lubrication systems, vibration levels, and other critical components. Timely identification of wear or abnormal operating conditions can help prevent unexpected breakdowns and maintain consistent separation performance.
Selecting the Right Centrifuge Machine
The selection of a centrifuge machine depends on various factors, including process capacity, feed characteristics, particle size, solids concentration, liquid properties, required separation efficiency, operating temperature, and desired output quality.
Understanding the application requirements helps determine the suitable centrifuge type, configuration, operating speed, and capacity. We can assist in evaluating process requirements and identifying a suitable centrifuge solution for specific industrial applications.
Reliable Centrifuge Solutions for Industrial Applications
Whether you require solid-liquid separation, sludge dewatering, clarification, process recovery, or other industrial separation requirements, our Centrifuge Machines are designed to provide efficient and dependable performance.
With suitable equipment selection, proper operation, preventive maintenance, and technical support, centrifuge systems can help improve separation efficiency, reduce processing requirements, minimize downtime, and support consistent plant operations.